

Gantry Machining Center Acceptance: Testing Accuracy Across Full Travel
A gantry machining center can satisfy an accuracy check near the table center while exceeding tolerance near an axis limit or at extended ram positions. Acceptance should therefore establish performance across the agreed working envelope, not merely confirm a favorable result at one convenient location. A positioning report alone does not prove that the tool will remain correctly located relative to the workpiece throughout that envelope.
The acceptance basis must connect positioning accuracy, geometric alignment, thermal behavior, and representative machining performance under documented conditions. Each addresses a different source of error; none substitutes for the others. A machine that repeats consistently can still position incorrectly, while accurate individual axes can still produce distorted features if their geometric relationship is wrong.
Define what “full travel” means before testing
The contract should identify the usable travel to be accepted, including any restrictions associated with spindle heads, tool length, fixtures, or rotary attachments. Nominal axis stroke is not automatically a collision-free machining envelope. Likewise, a test confined to the central portion of an axis cannot substantiate an unrestricted full-travel claim.
Record the coordinates of the test range, measurement lines, target positions, and relevant machine configurations. For a long-travel gantry, this includes where the saddle sits across the bridge and how far the ram extends. These positions change the relationship between the measuring line, guideways, and tool center point.
Full-travel verification does not mean measuring every possible point. It means using an agreed sampling plan over the entire accepted range, supplemented where necessary by additional measurements at travel extremes, support transitions, or production-critical locations. If safe overrun for bidirectional measurements limits the tested range, that limitation belongs in the acceptance record.
Use standards as test methods, not automatic tolerance guarantees
The ISO 230 series provides a framework for machine-tool testing. ISO 230-1 addresses geometric accuracy under no-load or quasi-static conditions; ISO 230-2 addresses positioning accuracy and repeatability of numerically controlled axes; ISO 230-3 addresses thermal effects. The applicable parts of ISO 10791 add machining-center-specific test provisions. ISO 10791-2 concerns machines with vertical spindles, but its configuration and scope must be checked against the machine being accepted.
A reference to “ISO accuracy” is incomplete without the standard part, edition, applicable tests, deviations from the method, and acceptance limits. General test codes explain how to measure and evaluate performance; they do not supply a universal tolerance for every gantry size and application. Where a machine-specific standard provides tolerances, the contract should identify which apply.
Factory acceptance and site acceptance also need a defined relationship. Transport, foundation conditions, leveling, and utility connections can change installed performance. A factory report is useful baseline evidence, but it does not by itself establish accuracy after installation.
Measure positioning in both directions across the accepted range
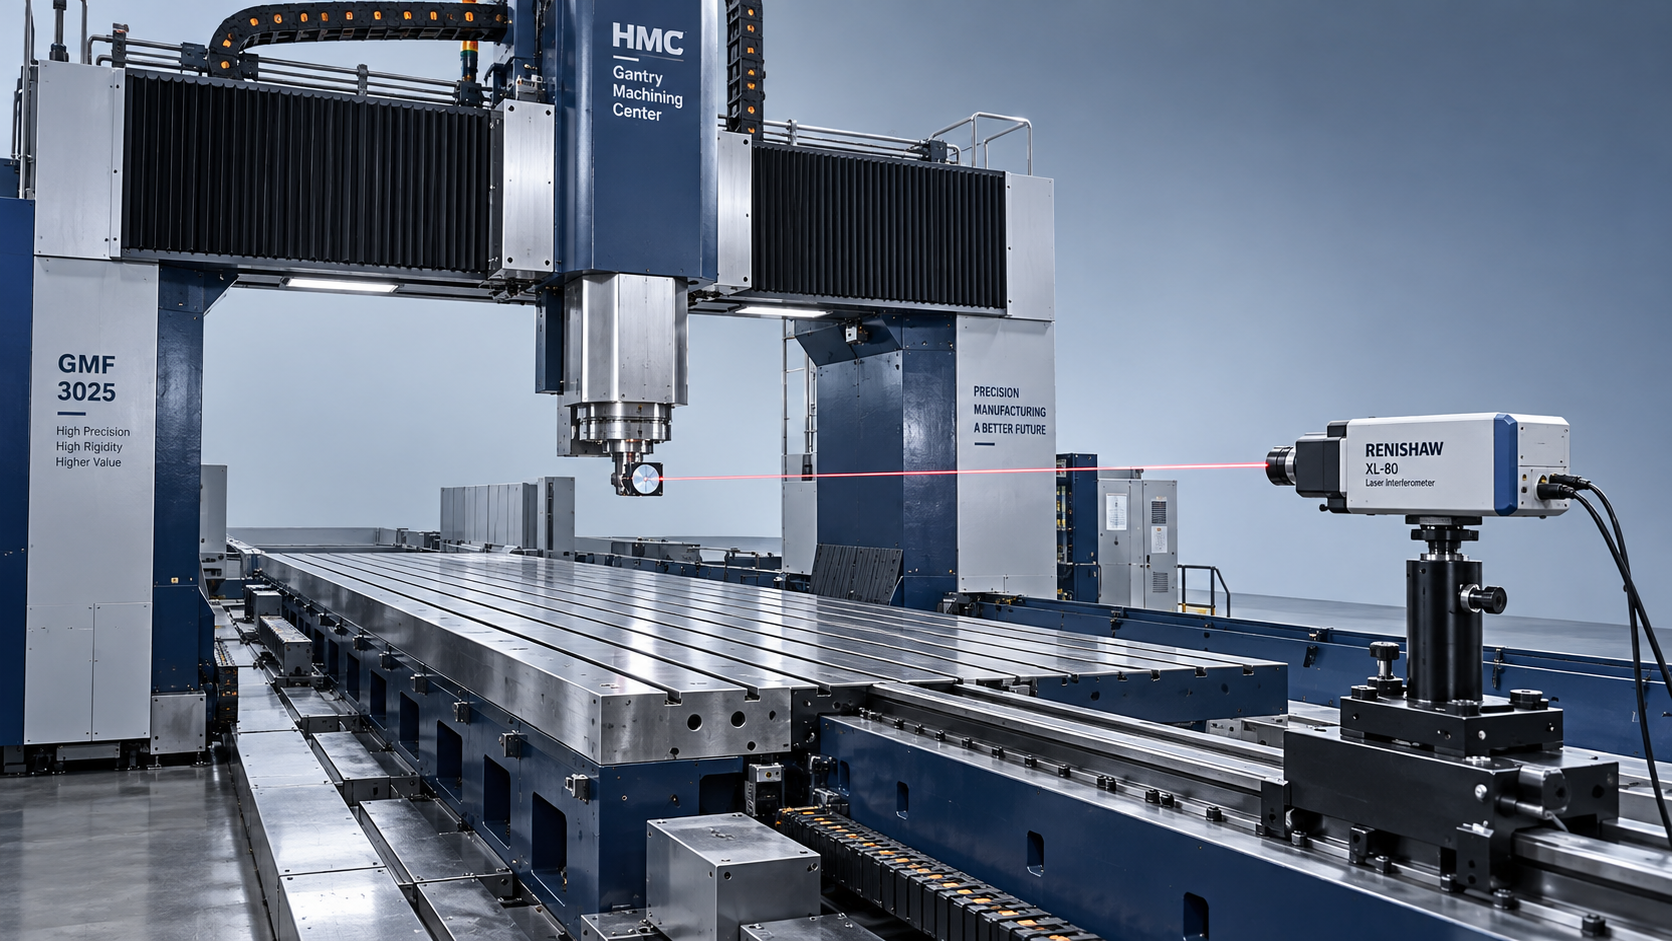
For linear-axis positioning tests, a calibrated laser interferometer can compare commanded movement with measured displacement along the measurement line. The setup must control alignment error and account for environmental influences on the measurement. Instrument calibration alone does not establish the uncertainty of the complete test.
Use target positions distributed according to the selected method, with repeated approaches from both directions. Follow the prescribed sampling and evaluation rules rather than replacing them with a small set of convenient stops. Supplemental targets can investigate local behavior, but should be distinguished from the standard test sequence.
Retain individual readings and position-by-position plots, not only a headline result. A single reported value cannot show where deviations occur or whether they follow a smooth trend or an abrupt local change. Record compensation settings and the relevant controller configuration. Any correction made during acceptance should be followed by a documented retest.
Check geometry where the tool actually works
An interferometer aligned along one axis measures displacement along its beam; that result does not independently establish straightness, angular motion, squareness, or spindle alignment. These require appropriate geometric measurements. On a gantry, pitch or yaw can create tool-point errors that increase with the distance between the measurement line and the cutting point—the practical consequence of an Abbe offset.
Geometry checks should therefore include configurations representative of use: positions along the bed, saddle locations across the bridge, and relevant ram extensions. A short, retracted ram can give a favorable result that does not represent deep machining. For machines with synchronized gantry drives, assess synchronization and bridge alignment through the manufacturer’s approved procedure; do not disable protective functions to create a test condition.
Define each geometric measurement by its reference, direction, and configuration. “Straightness checked” is insufficient without identifying which axis moved, which plane was measured, and where the other axes were positioned. Squareness checks must likewise identify the axis pair and measurement span.
A representative cutting test can then assess combined machine behavior. Use a documented workpiece, fixture, tool, cutting process, and inspection method. Features distributed over a large component or several table locations provide different evidence from a small central test piece. Cutting results supplement geometric tests; tool deflection and process variation prevent them from isolating machine error on their own.
Make thermal state and load explicit
“Machine warmed up” is not a reproducible test condition. Define spindle speeds, axis motion, coolant operation, warm-up duration, and the criterion for beginning measurement. Record ambient conditions and relevant machine temperatures throughout the test, particularly where gradients or changes could affect a long structure.
A baseline accuracy check and a thermal-drift test answer different questions. The former evaluates performance in a defined state; the latter tracks changes as operating conditions evolve. Where production involves sustained spindle operation or repeated long-axis movements, an agreed thermal test can reveal displacement that a short, stabilized inspection misses.
State the loading condition as well. No-load geometric acceptance does not establish performance under every permitted workpiece mass. If heavy or unevenly distributed loads are central to the application, agree on representative load cases and their locations before testing. Keep them within the machine’s specified limits.
Protect the test area without compromising the evidence
Full-travel testing brings moving structures close to instruments, cables, fixtures, and access boundaries. Review the complete motion path, including reversal and overrun distances, before executing the sequence. Secure measurement equipment and route cables outside pinch and crush zones.
Use the manufacturer’s approved setup mode and safeguarding procedures. Where installation or adjustment exposes personnel to hazardous motion or stored energy, apply the required isolation procedure. Do not defeat interlocks simply to obtain optical access. Emergency-stop access and an exclusion zone remain necessary during automated measurement.
Make acceptance a traceable decision
The final record should connect every result to the machine configuration, method, limit, and test conditions. Include machine identification, installation and leveling status, instrument traceability, measurement uncertainty, raw data, environmental records, compensation settings, deviations from the agreed procedure, and signed dispositions.
Agree in advance how measurement uncertainty affects conformity decisions. A result close to a limit should not be passed by rounding alone. If an axis, configuration, or operating condition fails, define the correction and retest scope; repeat related checks where the adjustment could have affected geometry or compensation.
Restricted acceptance is defensible only when its boundaries are explicit and enforceable. A machine accepted over a reduced envelope must not be recorded as meeting unrestricted full-travel requirements. The decisive evidence is a traceable set of results showing where, under what conditions, and against which criteria the machine meets its obligations.

Vedon
Typically replies within minutes
Any questions related to Home?
Elaine / Sales Director
Jaye / Sales Manager
Jessica / Sales Manager