Comparing Milling Machine Supplier Quotes Beyond the Base Price
Comparing Milling Machine Supplier Quotes Beyond the Base Price
The lowest milling machine quotation can become the more expensive purchase before the first production batch is complete. Missing toolholders, site preparation, commissioning travel, and an unsuitable spindle configuration can all change the economics. The useful comparison is not simply machine against machine. It is the cost of bringing each proposed system into dependable production—and keeping it there.
A milling machines supplier should make those boundaries clear. Procurement needs enough detail to distinguish a genuinely competitive offer from one that transfers costs and responsibilities to the buyer. Start with a common production requirement, then compare configuration, acceptance conditions, delivery scope, and operating costs on the same basis.
Make the quotations describe the same job
Two vertical machining centers with similar travels may not be equivalent purchases. One quotation may include probing, chip removal, and commissioning; another may cover only the machine in its standard configuration. Even an identical spindle power figure needs clarification: continuous and short-duration ratings are not interchangeable.
Give each supplier the same reference package: representative drawings, material grades, tolerance requirements, batch sizes, expected production hours, and the proposed workholding arrangement. Identify which requirements are mandatory and which are optional. Otherwise, suppliers may optimize their offers around different assumptions, leaving procurement to compare prices that answer different questions.
Read specifications through the workpiece, not the brochure
Travel and table dimensions are useful screening criteria, but they do not establish whether a part can be machined efficiently. Fixtures consume space and load capacity. Tool length affects clearance. A large component may fit on the table yet restrict spindle access or require additional setups.
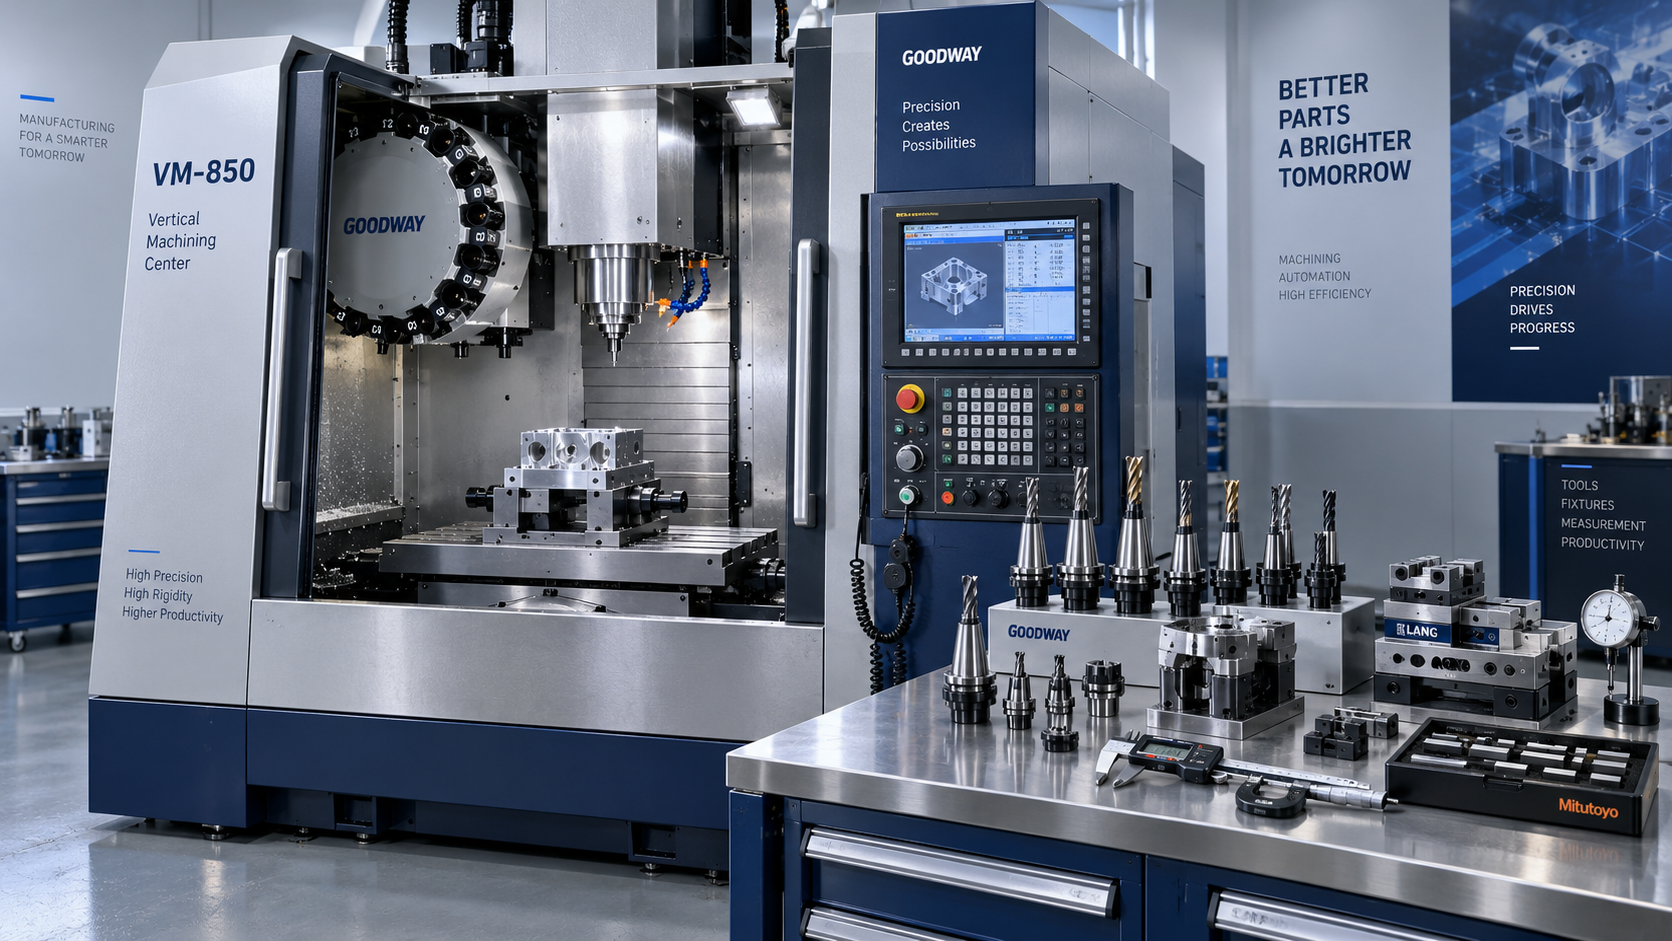
For example, the VMC1370 lists X/Y/Z travels of 1300/700/700 mm, a 1400 × 700 mm worktable, and a maximum table load of 1200 kg. These figures help establish an initial fit. The next check is the combined workpiece-and-fixture weight, the clamping layout, and tool access throughout the machining sequence.
Its listed 8000 rpm belt-driven BT40 spindle and 24-tool magazine also raise practical questions rather than settle the buying decision. Does the spindle suit the proposed cutter diameters and materials? Will the complete tool set fit without manual changes? Ask whether large-diameter tools require adjacent magazine positions to remain empty.
Accuracy deserves particular care. Positioning accuracy, repeatability, and finished-part capability describe different things. If specification sheets contain conflicting values or different measurement lengths, request a corrected, signed technical schedule. Agree on the test method, environmental conditions, and acceptance limits rather than choosing whichever figure looks most favorable.
Buy evidence of production capability
Rapid traverse speed and tool-change time do not establish production output. Actual cycle time includes cutting, loading, probing, chip clearance, inspection, and operator intervention. For thin-walled parts or complex surfaces, workholding, toolpath strategy, and thermal behavior may matter more than a headline speed.
Where the purchase risk justifies it, agree on a representative cutting trial. Record the material, tooling, fixture, machining program, inspection method, and resulting cycle time. A supplier demonstration using different material or relaxed tolerances should not be treated as proof of your production target.
Turn the agreed evidence into acceptance criteria. Define what will be checked before shipment and what must be confirmed after installation. If a test fails, the contract should explain the correction process, retesting responsibilities, and implications for payment. Clear criteria are more useful than a general promise of “high precision.”
Separate landed cost from production-ready cost
Freight is only one part of getting a machining center onto the shop floor. Confirm the named delivery location and agreed trade terms, then identify responsibility for insurance, import clearance, applicable duties, unloading, rigging, and positioning. Tax treatment and regulatory requirements depend on the destination and should be checked locally.
Site readiness is another common gap. Obtain the installation requirements before ordering: electrical supply, compressed air, foundation conditions, access dimensions, and service clearances. Confirm whether transformers, foundation work, coolant, and initial lubricants are included or buyer-supplied.
Delivery dates also need a defined endpoint. “Ready for shipment” is not the same as installed and accepted. Build the schedule around drawing approval, manufacturing, pre-shipment inspection, transport, commissioning, and operator training. Ask what prerequisites could delay each milestone and who is responsible for resolving them.
Price the support arrangement, not just the warranty period
A warranty has limited value if its scope is unclear. Establish when coverage starts, which components are covered, and whether labor, travel, freight, and diagnostic work are included. Consumables, wear items, and damage linked to maintenance or operation need explicit treatment.
After-sales service should be equally specific. Ask how faults are diagnosed, which support hours apply, and how replacement parts are sourced. Separate a response commitment from a repair commitment: acknowledging a fault does not mean the machine will be running again within the same period.
Training scope affects operating cost as well. Basic control instruction may not cover setup verification, preventive maintenance, alarm diagnosis, or process development. Identify the people being trained, the training location, and the tasks they should be able to perform afterward.
Make the final comparison auditable
Use one ownership period for every proposal. Add the purchase price, required options, logistics, site work, commissioning, tooling, training, and expected operating and maintenance costs; account for residual value where appropriate. Keep uncertain downtime assumptions visible and test alternative scenarios rather than presenting them as established facts.
Shandong VEDON Intelligent Equipment Co., Ltd. combines R&D, manufacturing, sales, and service across CNC machine tools, intelligent manufacturing solutions, and precision cutting tools. That scope provides a useful basis for discussing the machine, tooling, and integration together. The quotation should still identify exactly which elements are included and who owns each implementation task.
Before approving a milling machines supplier, request a revised offer that closes the remaining gaps: confirmed configuration, reconciled specifications, acceptance tests, delivery responsibilities, and service terms. The strongest purchasing decision is the one whose cost and production assumptions remain defensible after the machine arrives.

Vedon
Typically replies within minutes
Any questions related to Home?
Elaine / Sales Director
Jaye / Sales Manager
Jessica / Sales Manager